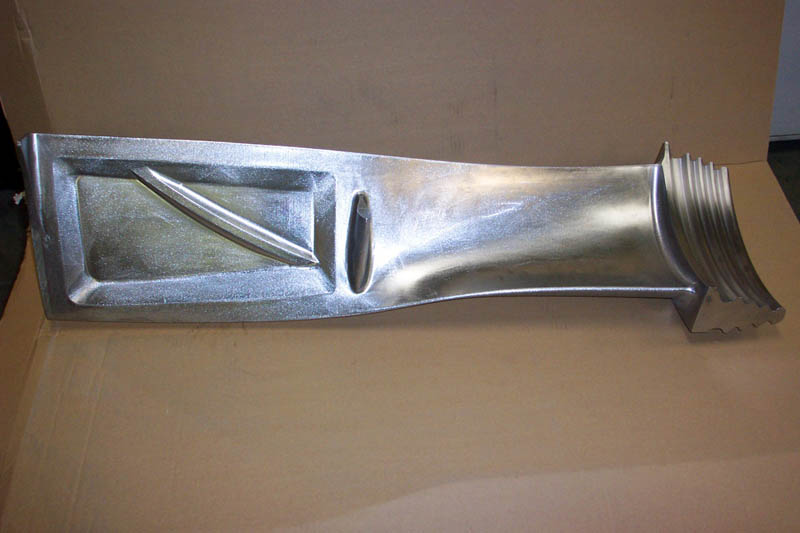
Turbine parts
For steam, gas and wind turbines, jet engines and fuel cells, in Hastelloy-X and Haynes 188.
A job shop in Clifton Park since 1983
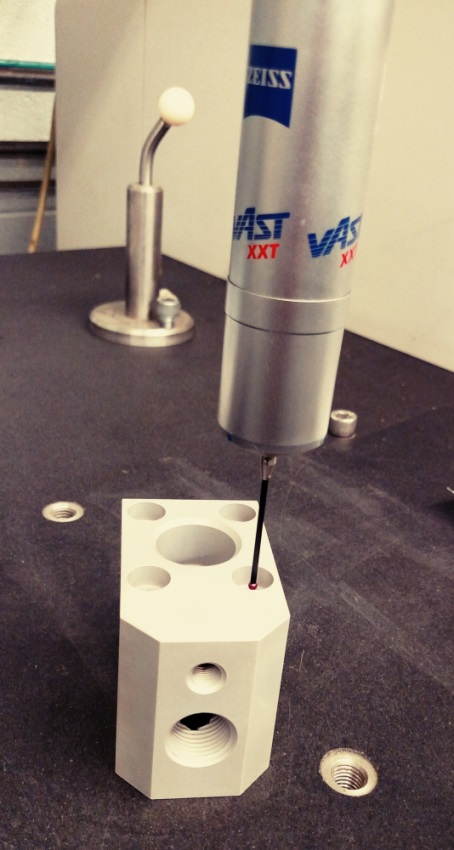
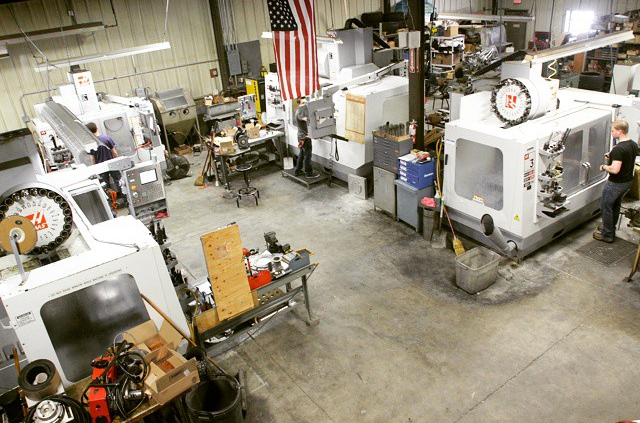
Prototype and production parts in titanium, Inconel and carbide, cut to 2 microns on five Fanuc wire EDMs, then milled, turned, ground and checked on a Zeiss CMM.
Five Fanuc Robocuts
±.00008 inHoles .012 to .118 in
4th axisMazak VCU-500A, 4 Haas
to 4,000 lbMazak QT Smart 250
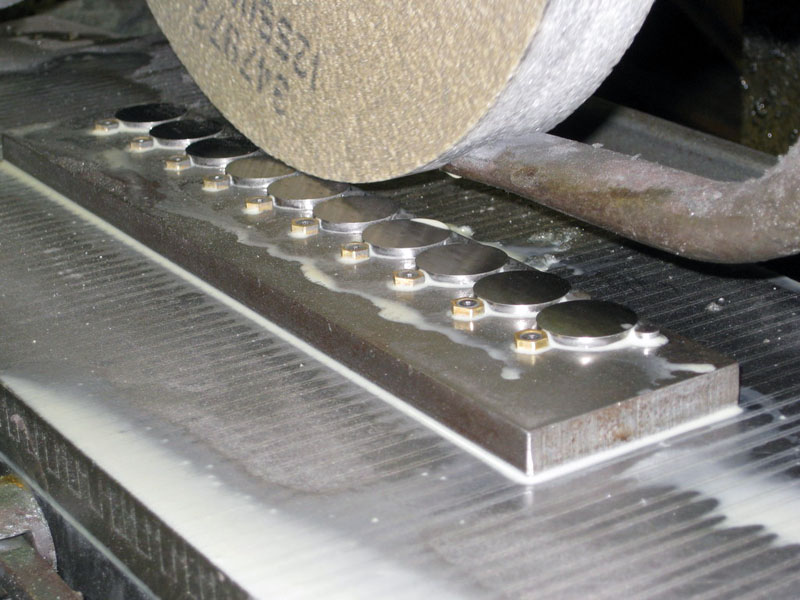
18.5 in swingSurface and cylindrical
under .0002 inZeiss Contura G2
27 × 40 × 24 in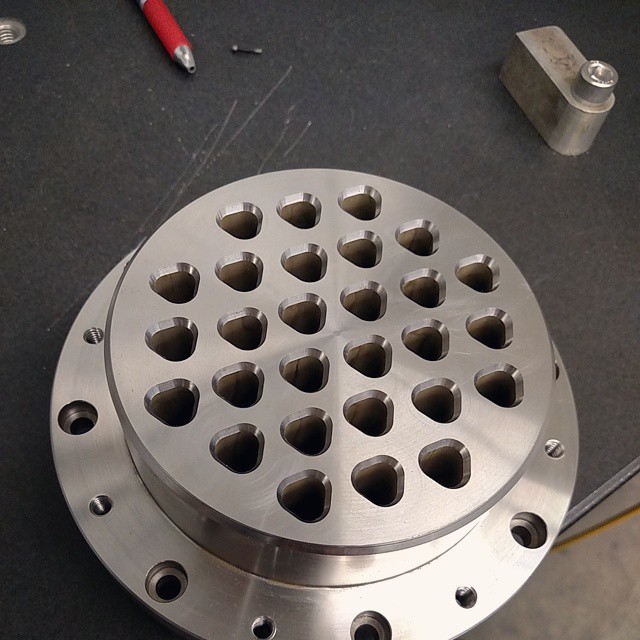
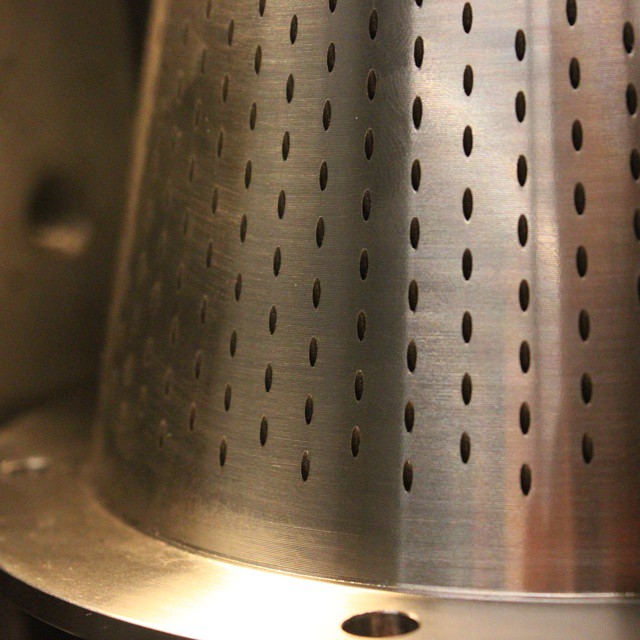
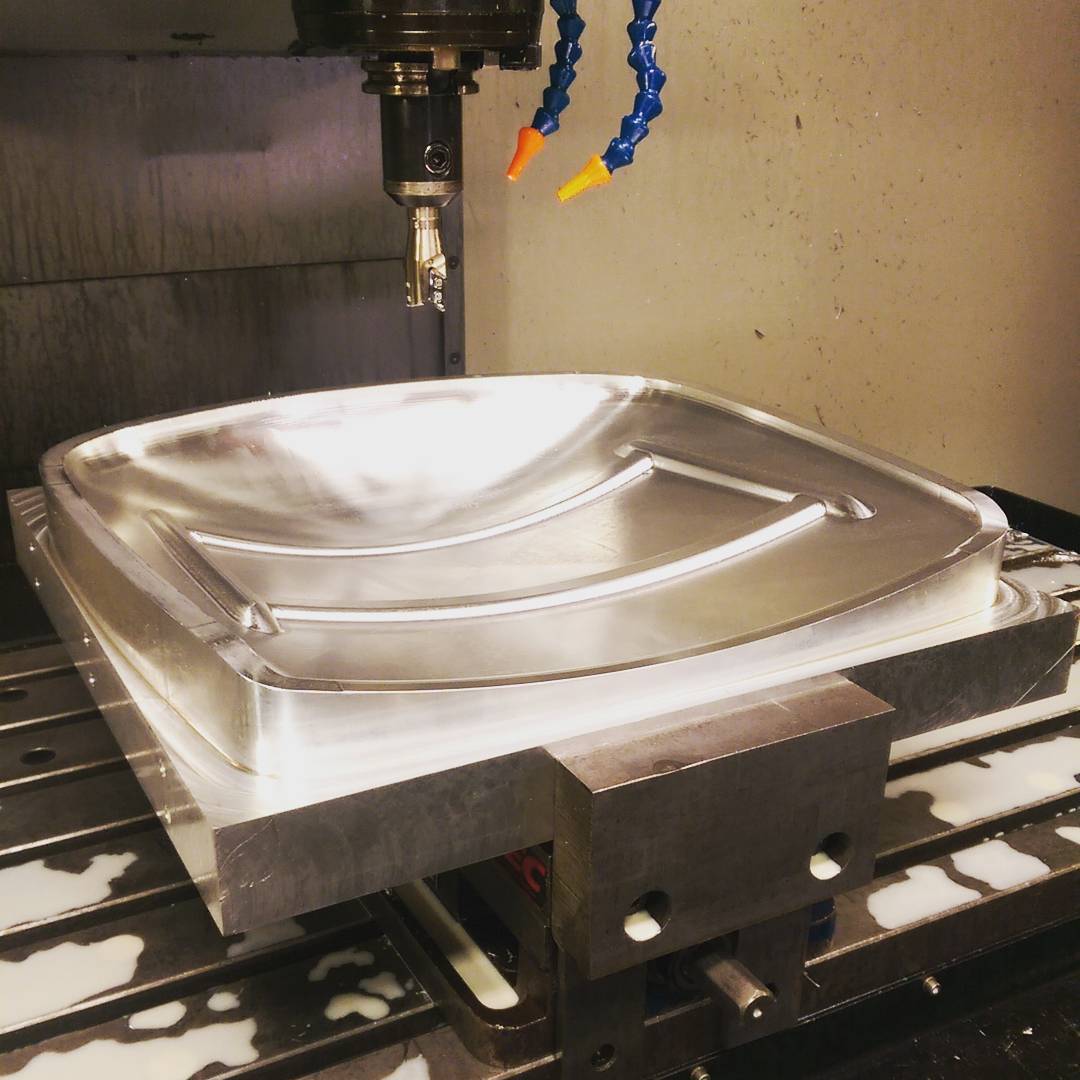
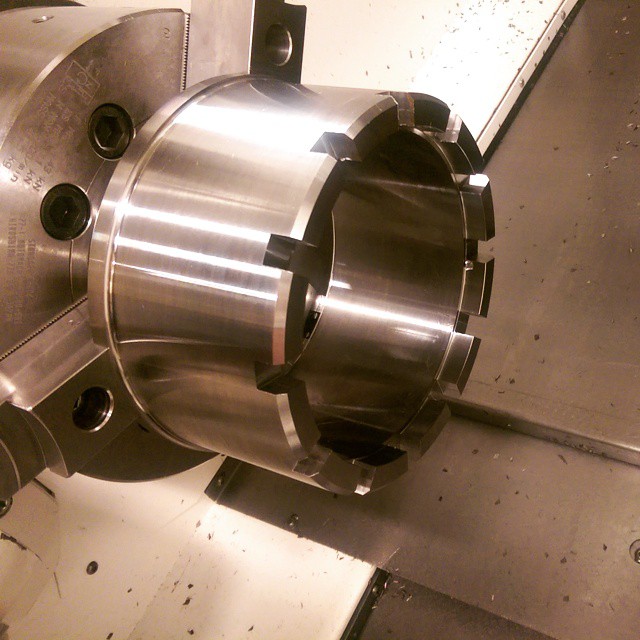
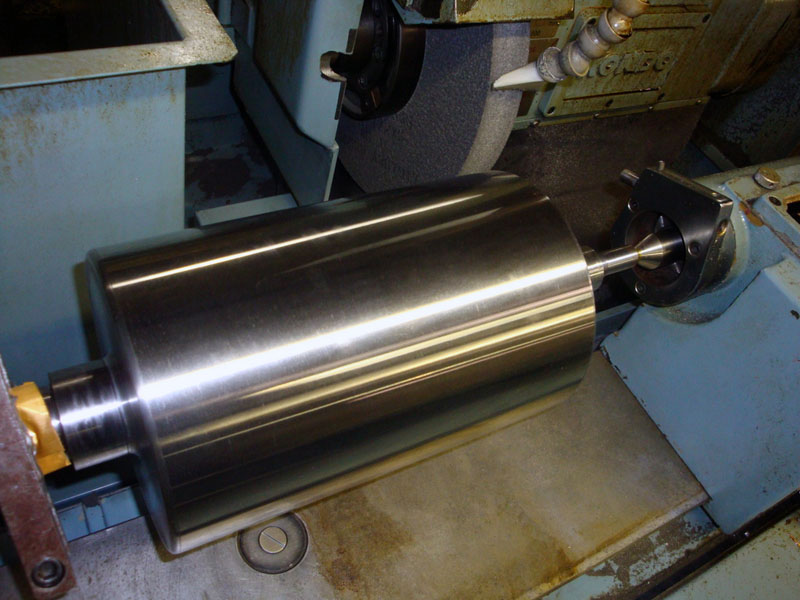
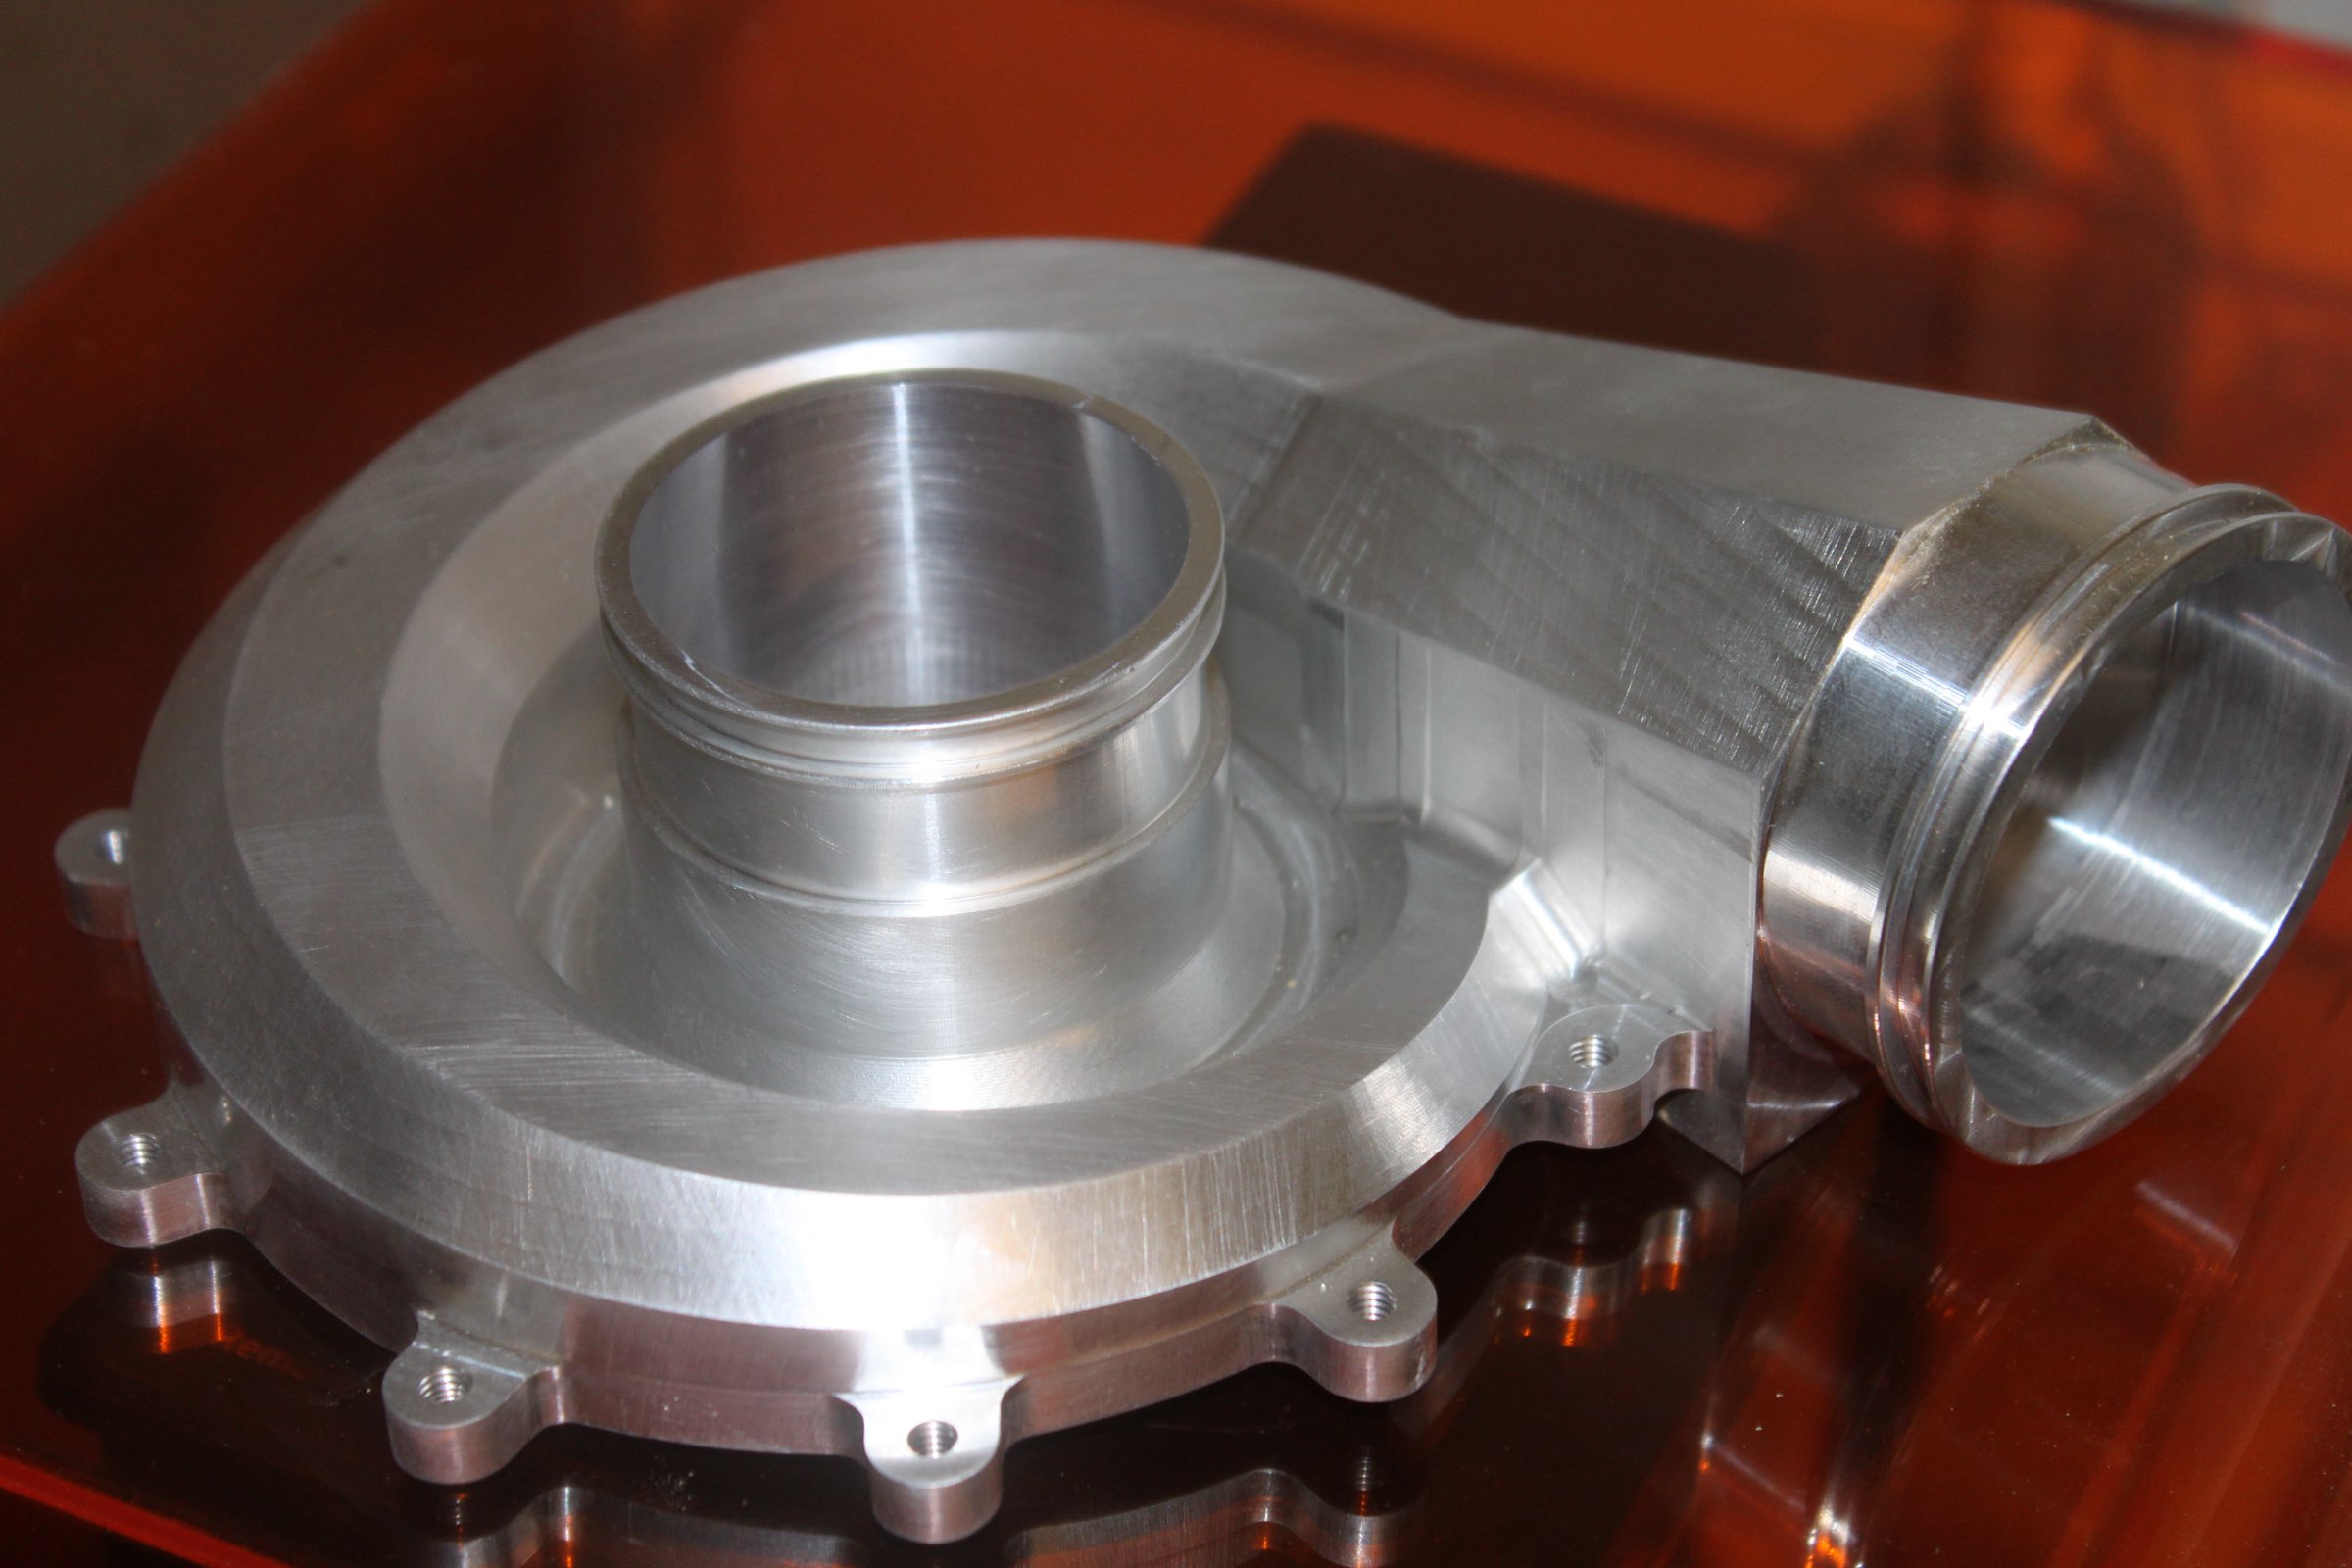
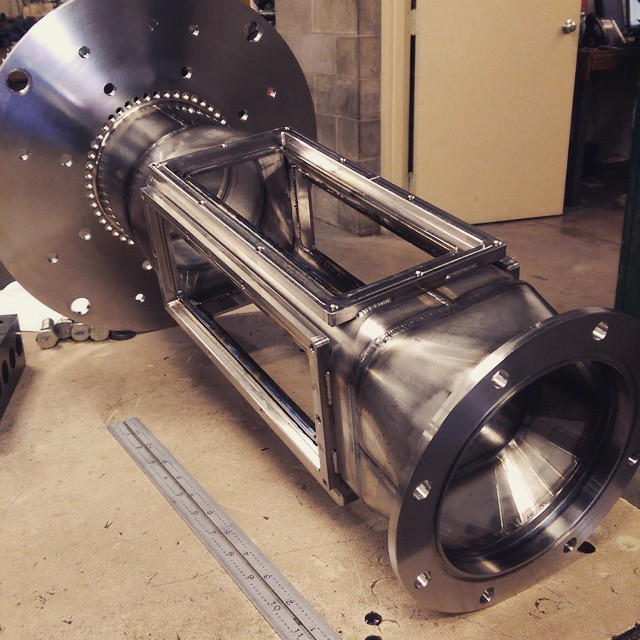
Each of these was made at AMT, as are aftermarket parts for 2,000 horsepower transmissions.
For steam, gas and wind turbines, jet engines and fuel cells, in Hastelloy-X and Haynes 188.
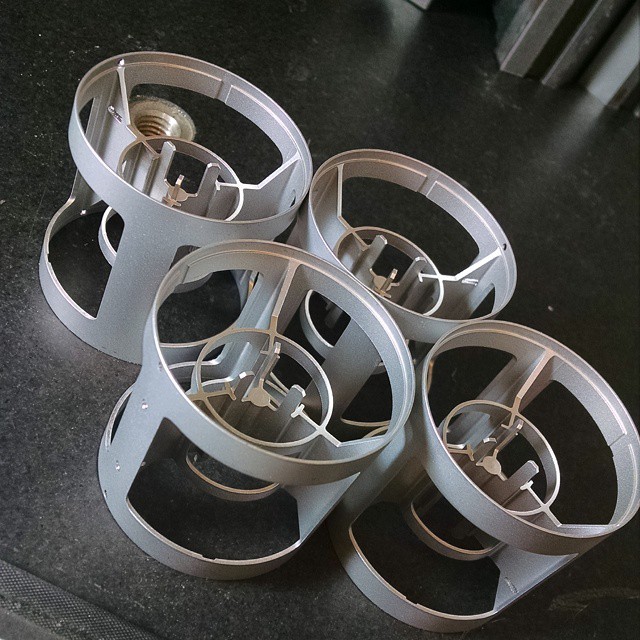
Held to ±.0001 in, alongside parts for X-ray optics and CT scanners.
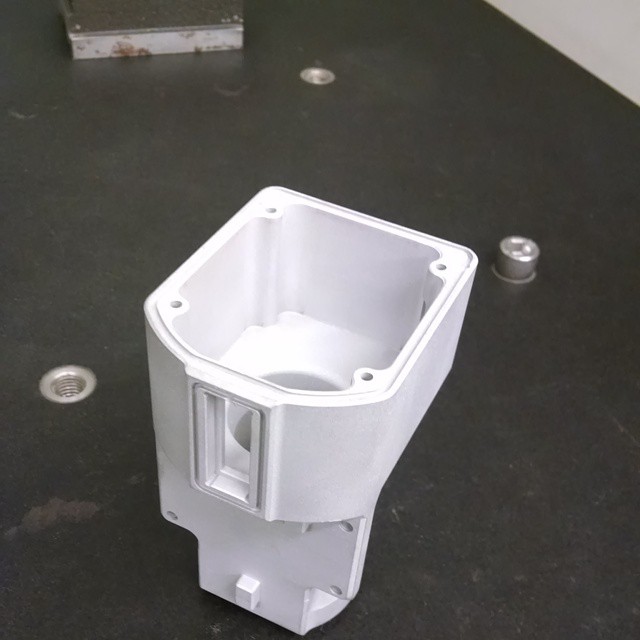
Tolerances under .001 in, with every part checked on the CMM.
PDF, DWG, DXF, IGES, STEP, Parasolid, SAT and Inventor files all open here.
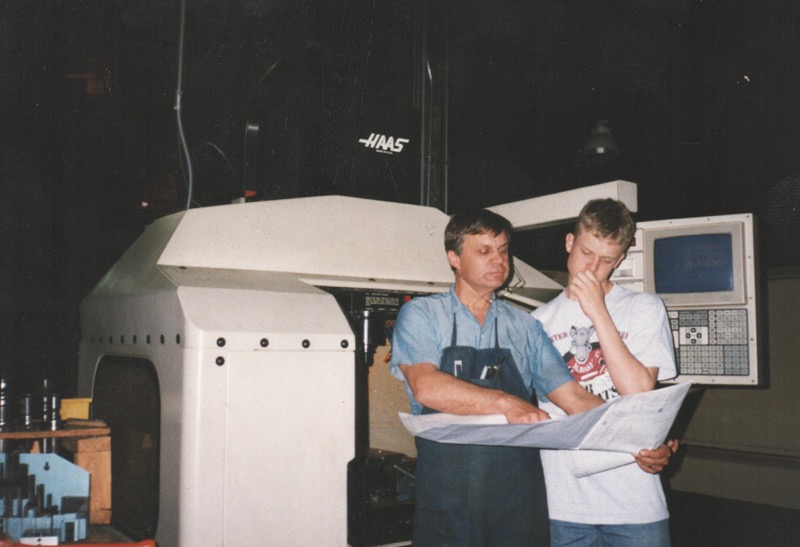
Esprit writes the toolpaths and E2 tracks the job through the shop.
The Zeiss Contura G2 checks the features on your drawing before the part leaves.
The answers engineers usually want before they send a drawing.
PDF, DWG, DXF, IGES, PRT, X_T, IPT, STP, STEP and SAT. Send a PDF drawing with the model when you can.
Wire EDM to 2 microns (.00008 in), grinding under .0002 in, and probed milling within .0001 in.
Any metal that conducts electricity, including titanium, carbide, Waspaloy, Hastelloy, Kovar and Inconel.
50 × 26 × 25 in, up to 4,000 lb.
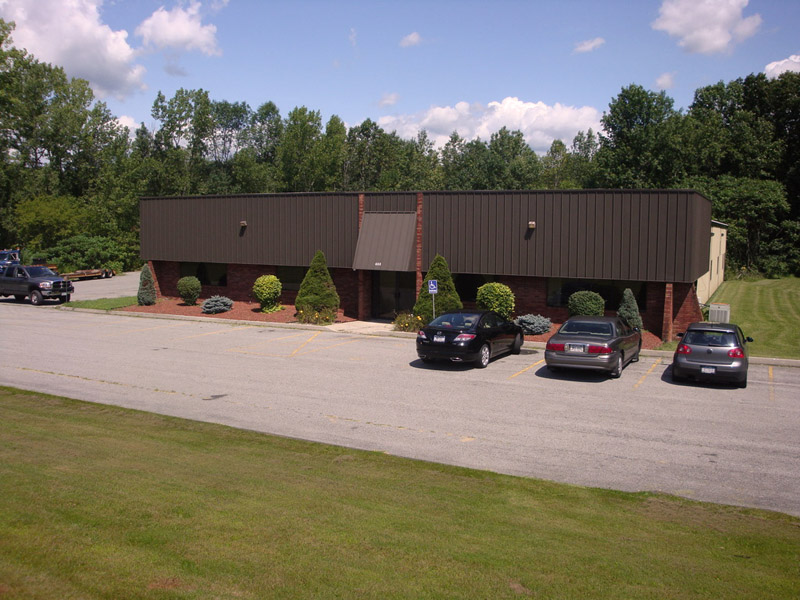
Steve Petronis and Dick Carusone started AMT in 1983 and moved it into this building five years later.
Tell us the part, the metal and how many you need.
Monday to Friday, 6 am to 4 pm